 Made in France
Manufacturing
Everything happens in Sissonne, in the Aisne
The body is blow-moulded, the parts injection-moulded, the artwork screen-printed and the bottles assembled under one roof. That is what holds the lead times — and what lets us re-run a batch without negotiating with anyone.
Sissonne, Aisne
A factory, not a buying office
The machines are ours, and so are the moulds. A cap designed fifteen years ago can be made again today, and a batch can be re-run without asking anyone — that is the difference between manufacturing and having something manufactured.
Manufacturing
100 % French, in fact 100 % Sissonne
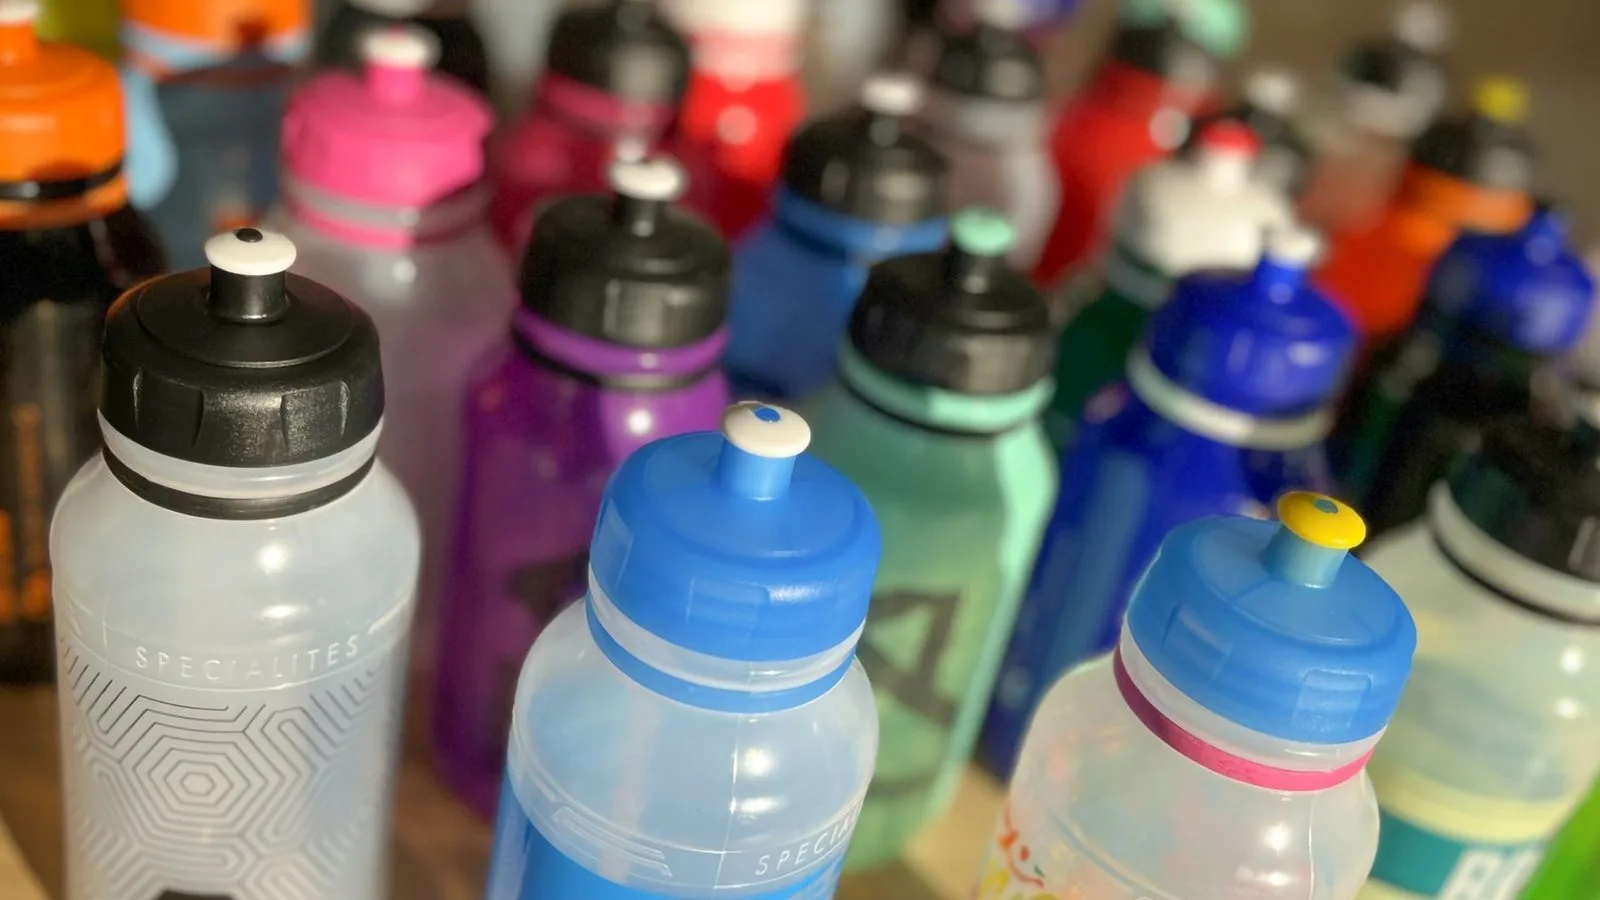
Many so-called French bottles are imported and then decorated in France. Here everything is under the same roof, in the Aisne: the material comes in as granules, the bottle goes out printed, assembled and packed. We blow the body, we injection mould the parts, we prepare our screens and we print — nothing is subcontracted.
The body
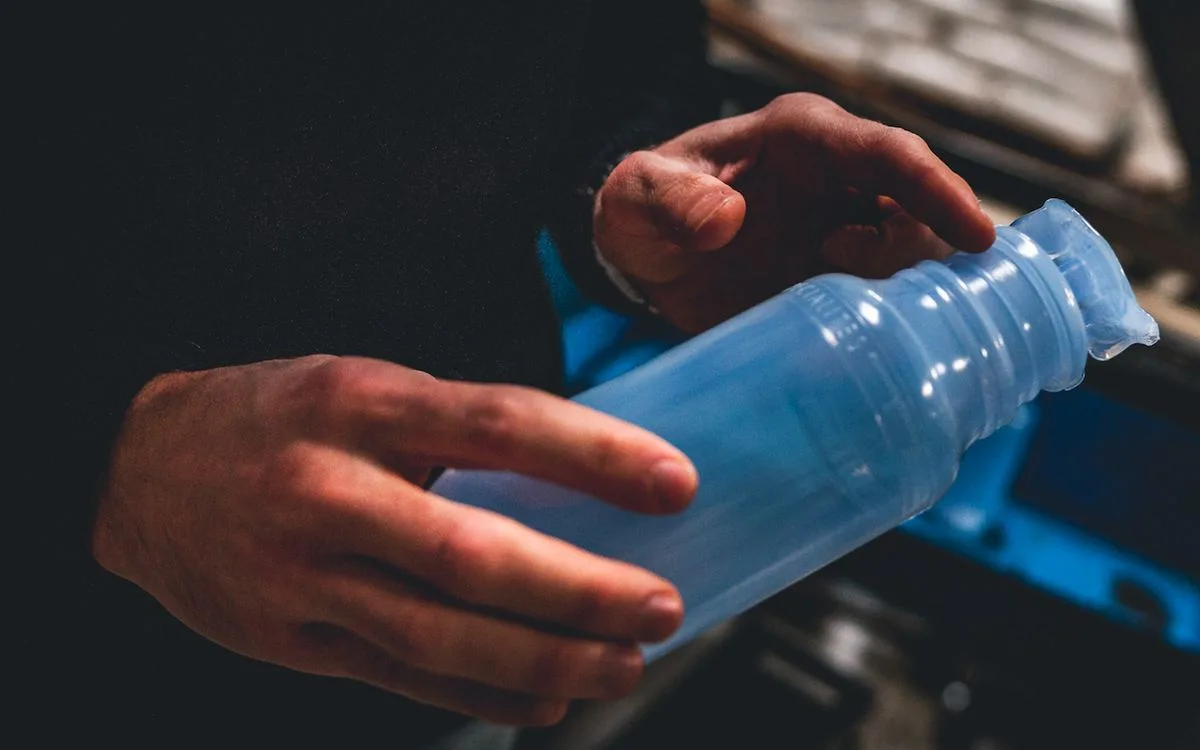
Extrusion blow moulding
The polyethylene is extruded as a parison then blown into the mould on our Sidel extrusion blow-moulding machines. It is that process which gives the bottle its soft wall — the one you squeeze to drink — and the Spécialités T.A. lettering embossed into the material.
The parts
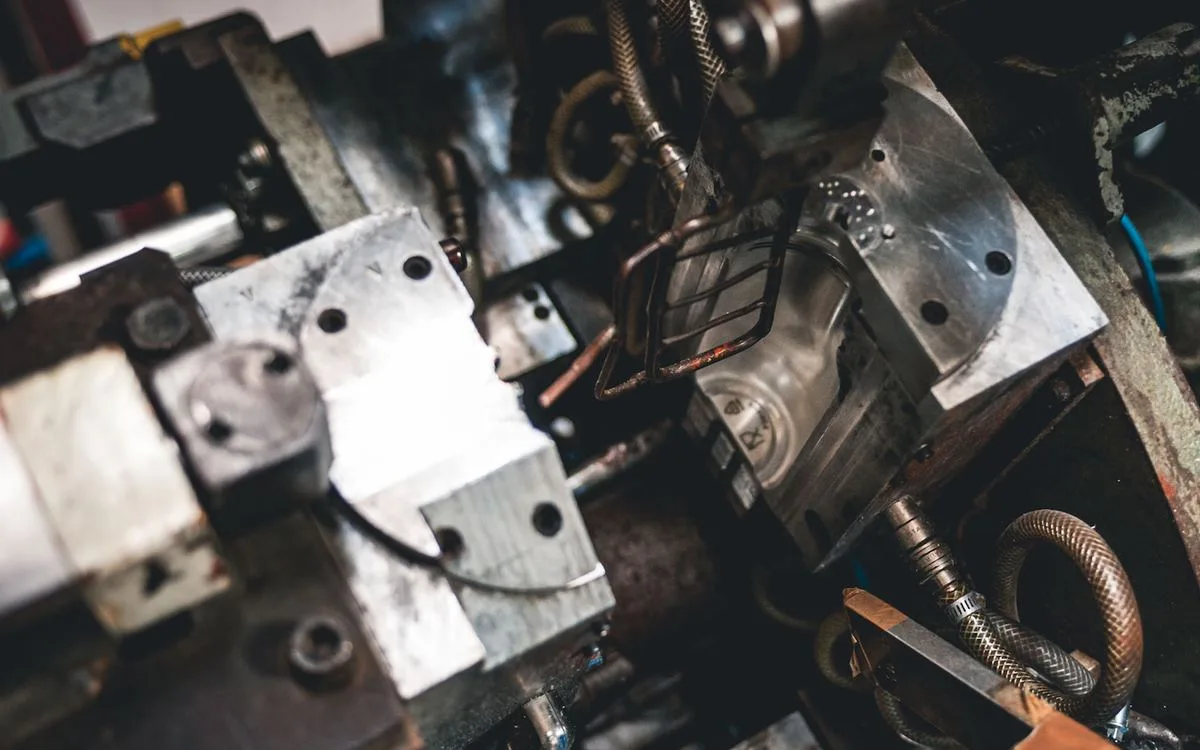
Plastic injection
The cap, the valve and the collar are injection moulded on our Sandretto presses. Each colour is a mass-dyed material: the colour cannot chip, it is in the part itself.
The proof and the screens
One screen per colour
Nothing is printed before the print proof is approved. The file is then separated colour by colour, and each colour receives its own screen, prepared in-house. It is that fixed work which explains the minimum of 125 bottles: the screens cost the same for 125 pieces as for 5,000.
The artwork
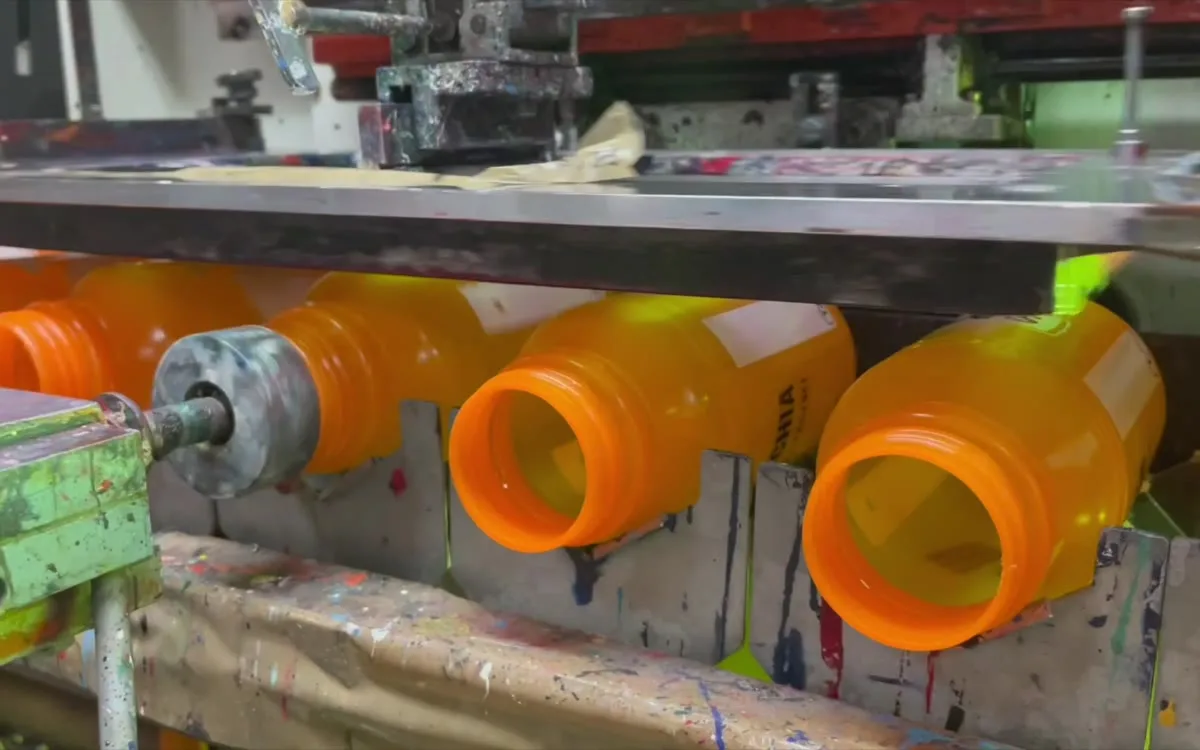
Screen printing
The screens are prepared and the inks laid down in our own workshops, colour by colour, right round the circumference. Nothing goes out to a printer: the same company blows the body and prints it.
Assembly
Assembly and shipping
Assembly of the four parts, inspection, packing and dispatch from the workshop. The bottle leaves Sissonne only once finished.
Spécialités T.A. workshop — 41 bis rue de Laon, 02150 Sissonne. Sidel machines (extrusion blow moulding) and Sandretto injection presses.
From screen to bottle
How a colour reaches the bottle
Four stages between your file and the ink on the bottle, all carried out in Sissonne. They repeat as many times as there are colours.
Colour separation
on a computer
Your file is separated colour by colour: one layer per ink, plus the white underlay if the body is dark. This is where the trapping is set; without it a sliver of bare bottle would show between two solids.
The film positives
layer output
Each layer is printed in opaque black on film. One positive per colour: it is the mask used to expose the screen.
Exposure
screen preparation
The film positive is pressed against a mesh coated with emulsion, then exposed to UV. The emulsion hardens everywhere except under the black: on rinsing, the design opens up and the ink will be able to pass. One screen per colour, prepared for your order.
The print run
with the squeegee
The bottle turns under the screen while the squeegee pushes the ink through the mesh. One pass per colour, with drying in between. It is that choreography that lays the design across the whole printable width.
In pictures
How your bottle is made
Printed work
What screen printing can do
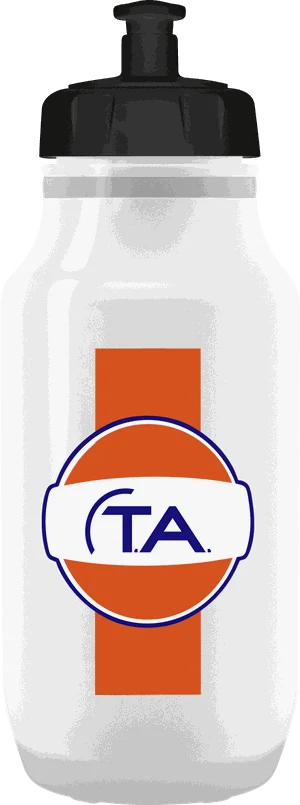
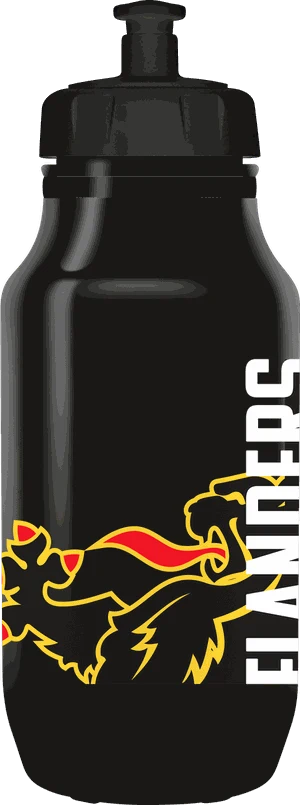
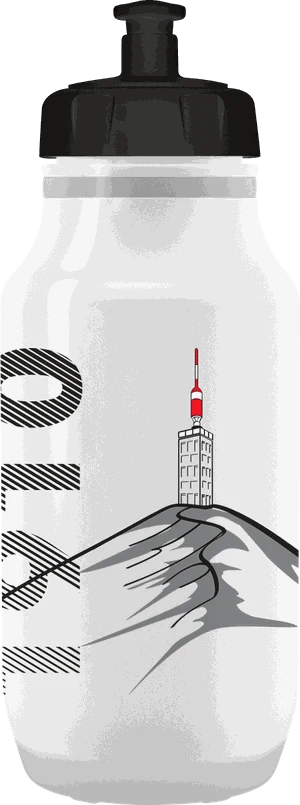
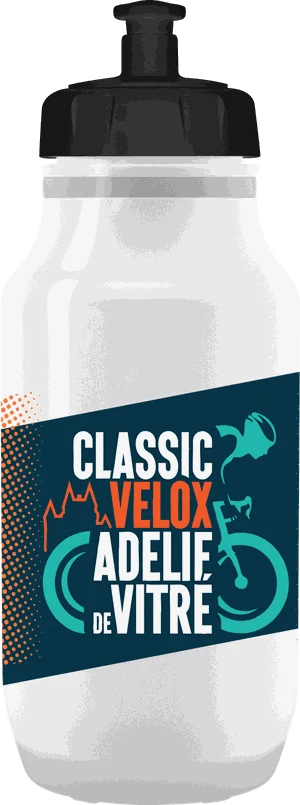
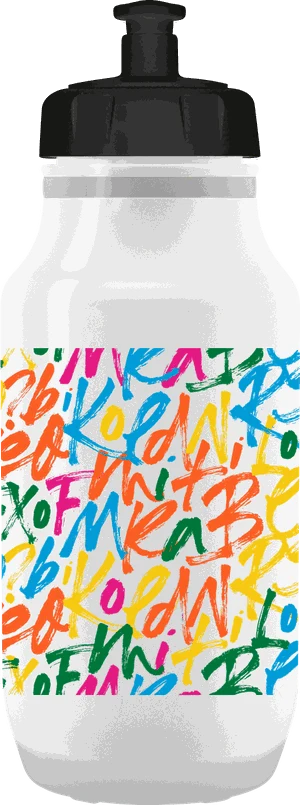
Designs actually printed in our workshop. A full pattern going right round, a halftone in place of a gradient, tight registration between colours, a white underlay on a dark body.
Try it with your artwork
The configurator wraps your file around the bottle and shows you the result from every angle. No account needed.